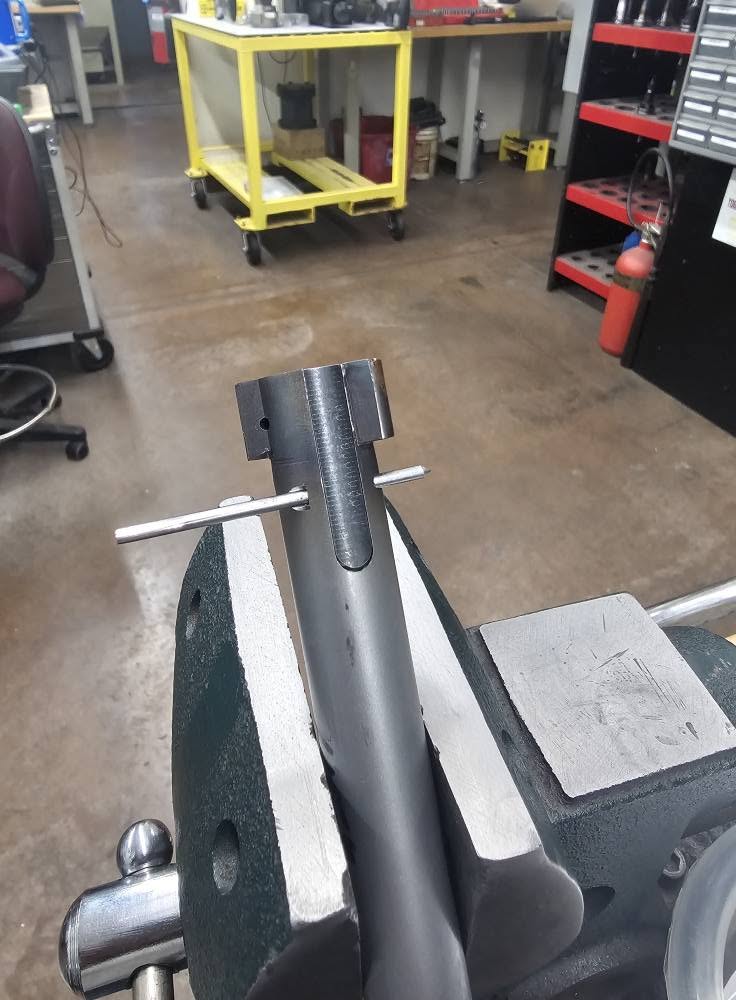
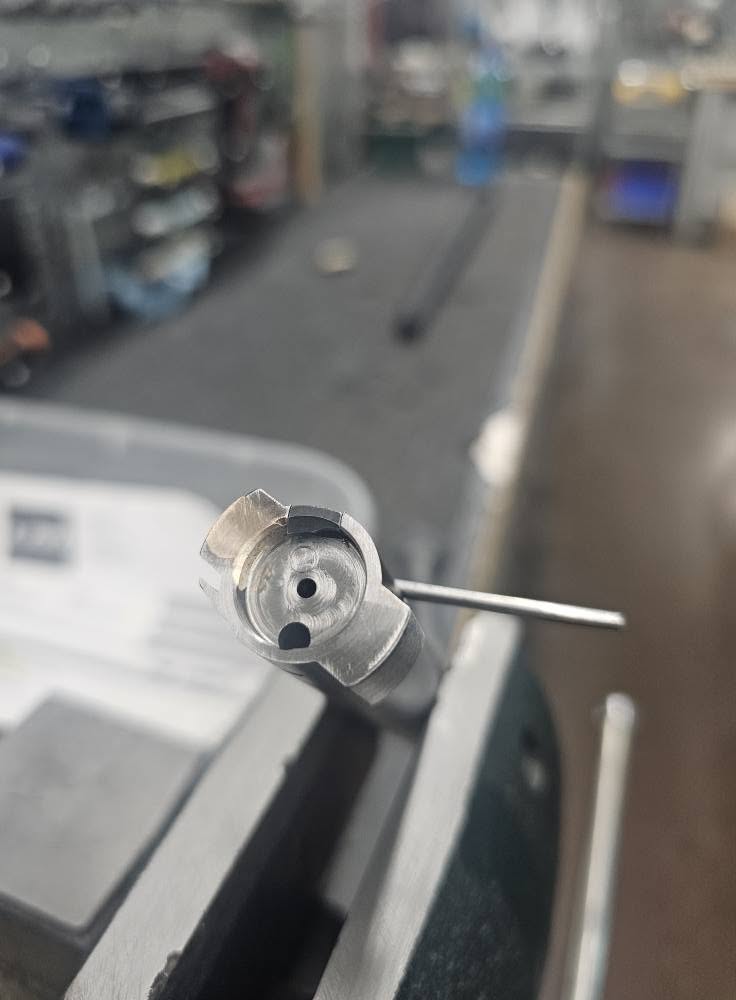
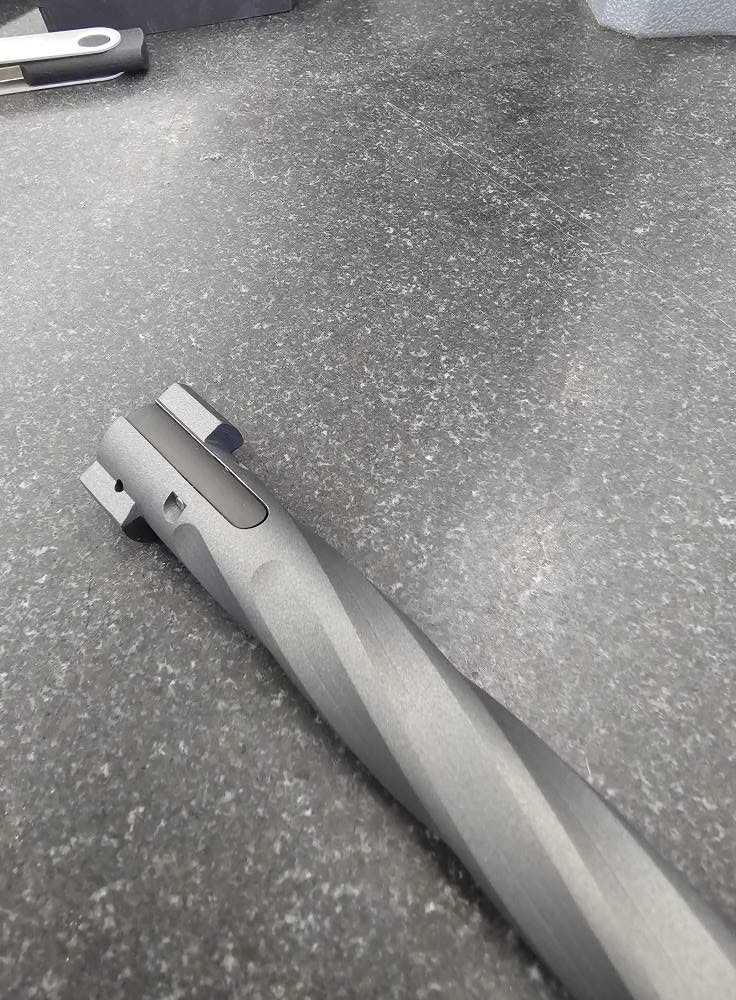
GUNSMITHING SERVICES: Winchester model 70 M16 extractor conversion
$275.00
Description
Winchester Post 64 Push Feeds
Winchester’s departure from the Mauser style, fixed extractor has mixed reviews among Winchester fans. We’ve seen that the T-slot design is prone to failure when cartridges become reluctant to come out of the chamber.
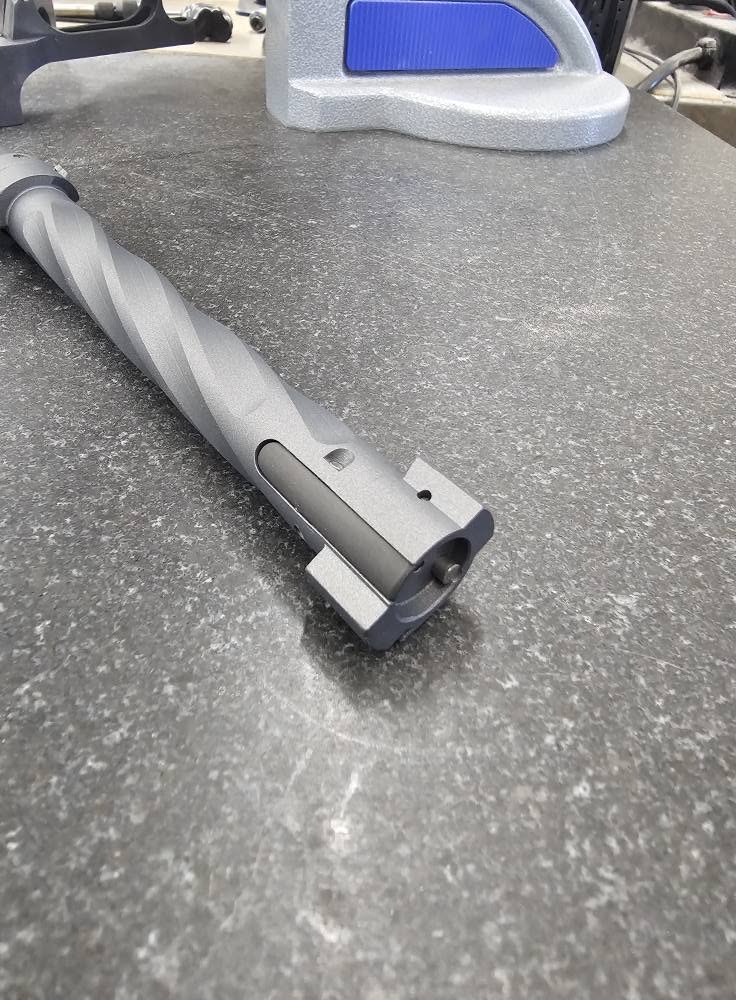
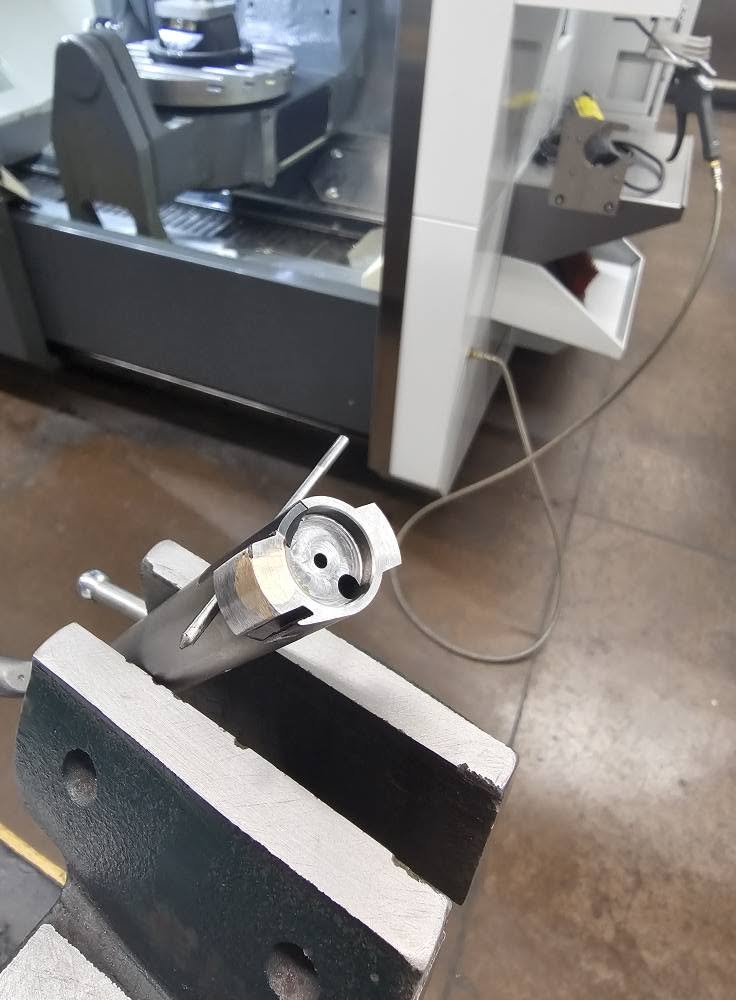
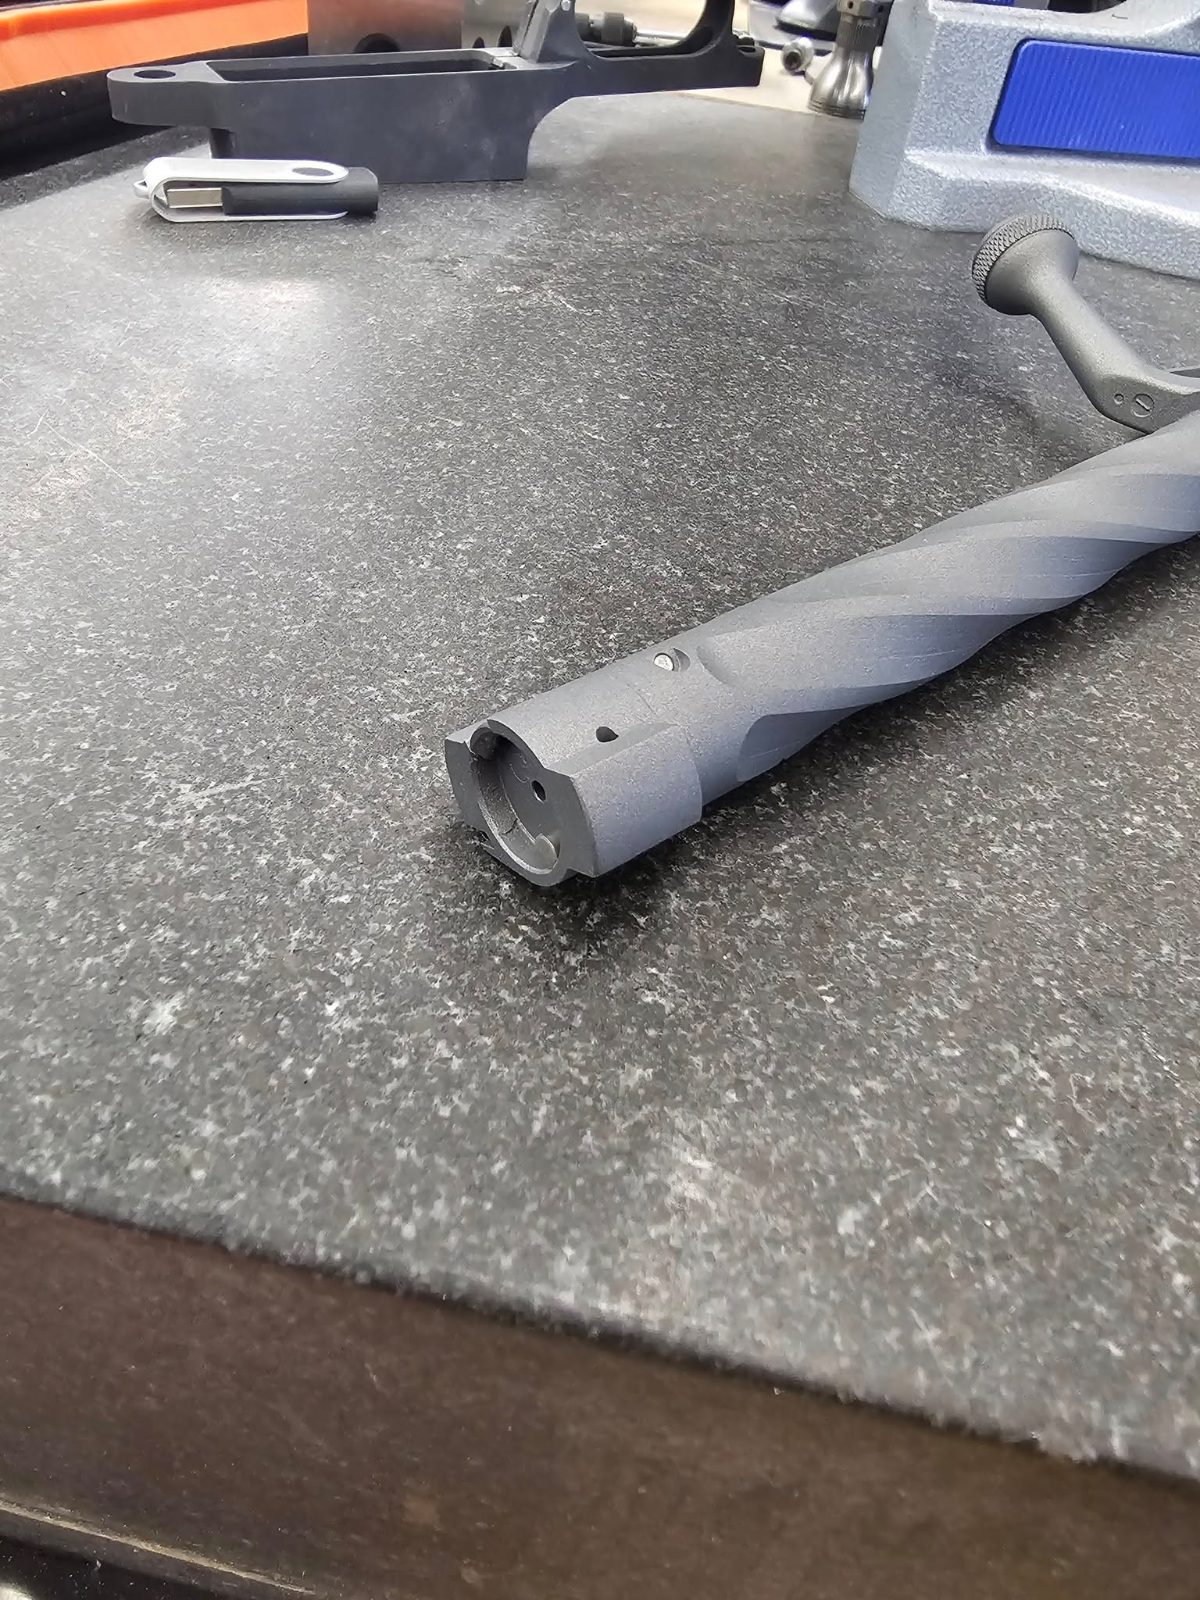
This design presents some unique problems to solve when converting to an M16 extractor. First is making the OEM ejector slot go away. Welding on a heat-treated part that endures tens of thousands of pounds of force as daily routine is not a trivial thing. We have successfully used silicon bronze brazing rod as it can be applied with a Tig Torch at a much lower temperature. The brazed surfaces only need to be warmed up. The filler rod is where the business end of a TIG torch is really applied. Additionally, use of heat absorbing paste along with an aluminum heat sink is used to preserve the tensile strength of the bolt head. Silicon bronze fills the void once occupied by the original extractor to ensure reliable function by capturing the head of the cartridge.
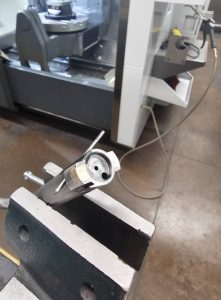
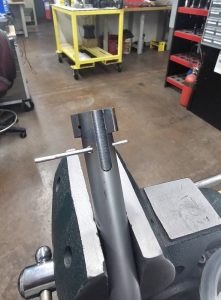
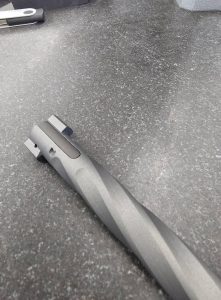
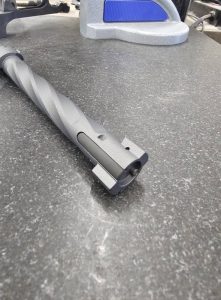
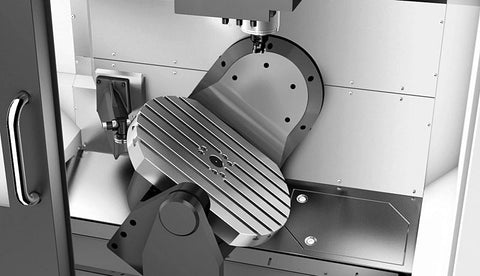
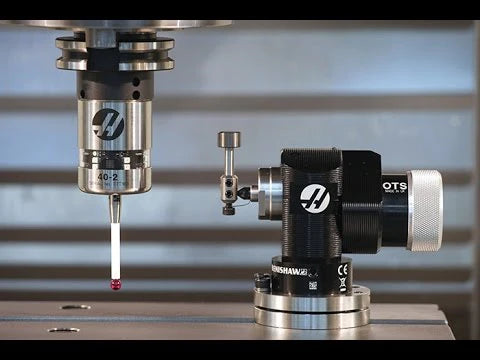
Once completed, the job can move to the mill for machining. Wireless electronic probing runs through a series of preprogrammed routines to locate and qualify the part so that all machining operations can consolidate into a single setup. 5-axis machining used this way is likely the largest leap this trade has seen in 30 years. We are fortunate to be the tip of the spear.
NOTE:
As a standard practice, the face of the bolt is resurfaced when installing the extractor. This removes any residual solder from the bushing installation. Your headspace will change between .0005″ and .001″. When fitting for a new barrel, it’s of no consequence as the headspace dimension is qualified during fit up. For reloaders, all that is required is maybe a small adjustment of your sizer die. For shooters using factory ammunition, there is no change. We understand the reluctance some may have with this. We ask you to trust the process and our judgement. Literally thousands of bolts have circulated through here. If there was an issue, we would have seen it by now.
M16 Extractors:
Many companies manufacture M16 type extractors for bolt action rifles. Within this community exists small, yet important differences. The larger issue we faced was availability. It helps no one if your project sits on a shelf for weeks because a 40-dollar part is out of stock.
Our extractors are 100% machined from tool-grade steel in-house. We do not use the sintered metal process to make any of our parts. The existing extractor design is quite good, but some small changes were made. Ours have a .005″ radius at the corners of the pawl to mitigate abuse to the case rim. We also added an included angle that “bites” the case rim groove for better retention. They are available in both R and L hand. We offer two sizes. The .187″ wide “mini” and our standard 6mm size.
We also offer these as a product available to purchase directly for shops who prefer to do their own work and for those wanting the peace of mind of having a spare.
Our 6mm extractors are compatible with both .480 and .545 bolt face cartridges (.308 and Standard Magnum). The .187″ wide “mini” extractor is for smaller diameter bolt faces.
M16 CONVERSIONS TO A .590″ BOLT FACE DIAMETER:
LRI will not convert any .700″ diameter bolt to a .590″ bolt face. Yes, we are aware that Remington once offered it. History also showed that to be a mistake. The use of 300+ grain projectiles combined with 60,000+ psi chamber pressures are outside the zone of what the actions are designed for.
People much more educated than we are did the homework. The data does not lie.
Additional information
| EXTRACTOR SIZE | MINI, .187", STANDARD AND MAGNUM, 6MM |
|---|---|
| DESIRED BOLT FACE DIAMETER | .390", .420", .450", .480", .550" |
| BUSHING MATERIAL | CARBON STEEL, STAINLESS STEEL |
Related products
-

GUNSMITHING SERVICES: Bolt jeweling
Price range: $100.00 through $175.00 Select options This product has multiple variants. The options may be chosen on the product page -

GUNSMITHING SERVICES: Receiver guard screw restoration/alteration
Price range: $125.00 through $215.00 Select options This product has multiple variants. The options may be chosen on the product page -

GUNSMITHING SERVICES: Barrel fluting
From $325.00 Configure -

GUNSMITHING SERVICES: Install timed muzzle brake-direct fit, no clamp/lock ring
$75.00 Add to cart